Few flooring products carry as much visual weight as chevron parquet. The continuous V-shaped pattern that runs the length of a room is what makes this product attractive to architects and hospitality designers, and it is also what makes every production error visible once the floor is laid. A slightly inconsistent mitre angle, a plank sorted into the wrong hand, or a moisture-driven dimensional shift will appear as a dark line across a lobby that was meant to look seamless.
This guide is written for distributors, general contractors, specifiers, and hotel or commercial project teams who need to evaluate a chevron parquet flooring supplier before committing a large purchase order. It does not explain the product from first principles. Instead, it sets out the technical distinctions, manufacturing tolerances, waste allowances, customization parameters, and compliance documents that determine whether an order will perform as specified.
DistributorsSpecifiersContractorsHotel ProjectsTender Teams
Five questions every buyer should be able to answer before ordering: Does the supplier understand the cutting geometry? Can the factory hold tolerances across every batch? Can the product be adapted to the project? Do the certificates meet the destination market? How are waste, lead time, and quality deviations controlled?
Chevron and Herringbone Are Not Interchangeable: The Geometry That Changes Your Order
How the joint geometry differs
Chevron and herringbone are often grouped together, but their manufacturing and installation implications are quite different. In both patterns, planks are arranged to create a zigzag rhythm, yet the way each plank is cut determines how much tolerance the finished floor can absorb.
Chevron: each plank is mitred at both ends, usually to a 45-degree or 60-degree angle. Adjacent planks meet point to point, so the joint has no overlap to hide small errors.
Herringbone: planks are rectangular with square ends. Each row is offset at a right angle, and the joint is a butt connection rather than a mitre, which makes the pattern more forgiving of minor dimensional variation.
For a buyer, this means chevron parquet requires a tighter production specification. The supplier must control angle accuracy, plank length, thickness, and edge profile with far less margin than a rectangular product would allow.
What the difference means for waste and budget
Mitred ends generate wedge-shaped offcuts. Because these pieces cannot easily be reused within the same pattern, the waste allowance for chevron parquet is significantly higher than for straight or herringbone layouts. Industry practice commonly places chevron waste between 15 and 25 percent, depending on room shape, plank length, and the number of pattern starting points.
15 to 25 percentTypical chevron waste allowance for budgeting
45 or 60 degreesCommon mitre angles in project supply
Two handsLeft-hand and right-hand planks must be sorted separately
Where each pattern fits
Pattern
Visual flow
Manufacturing difficulty
Typical waste
Typical project fit
Chevron (mitred 45 or 60 degrees)
Continuous directional V
High
15 to 25 percent
Hotel lobbies, showrooms, premium residential
Herringbone (square ends)
Zigzag rhythm
Moderate
10 to 15 percent
Classic interiors, offices, living areas
Straight lay
Linear and calm
Low
5 to 10 percent
Large open-plan spaces with tighter budgets
Manufacturing Tolerances That Separate Capable Factories From Risky Ones
A supplier's claim to produce chevron parquet is only meaningful if it can be verified against measurable production standards. Ask for written tolerance documents rather than verbal assurances, and request sample records from recent production runs. The areas below deserve the most attention during evaluation.
Angle accuracy and symmetry
The mitre angle is the single most important dimension in chevron production. Even a small deviation on each plank accumulates across a long run, producing visible drift in the V-pattern. Strong suppliers hold angle tolerance tightly and verify it with calibrated jigs or cutting stations at defined intervals. A 45-degree product and a 60-degree product require different tooling, so confirm that the factory can supply the exact angle your project specifies rather than the nearest available option.
Symmetry matters as much as absolute accuracy. Both ends of each plank must be cut consistently so that the pattern closes correctly at every joint. Ask how the factory checks symmetry between left-hand and right-hand cuts and whether it test-lays a sample section before full production begins.
Material and finishing consistency
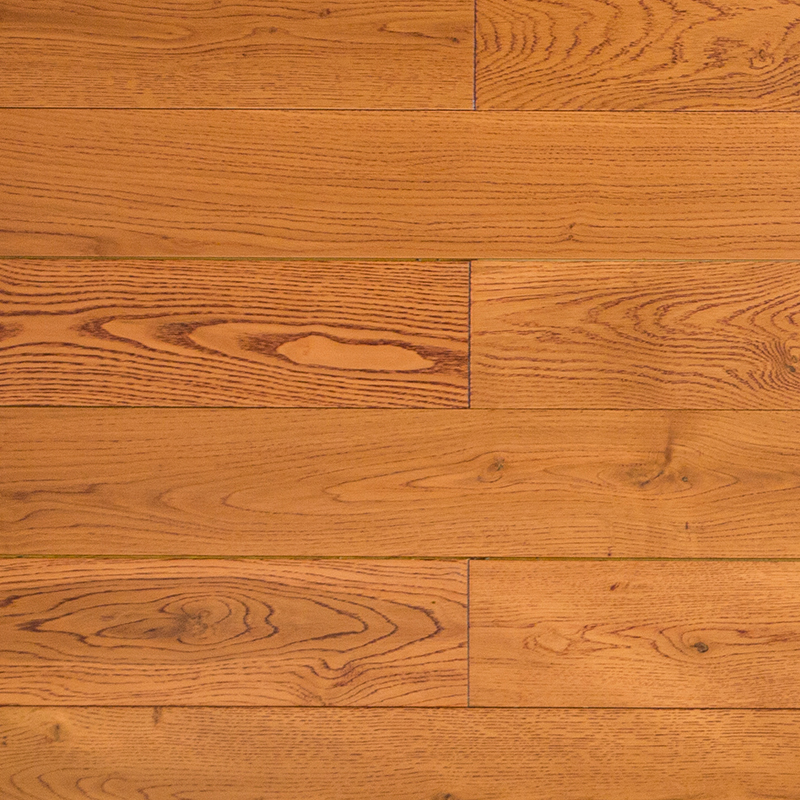
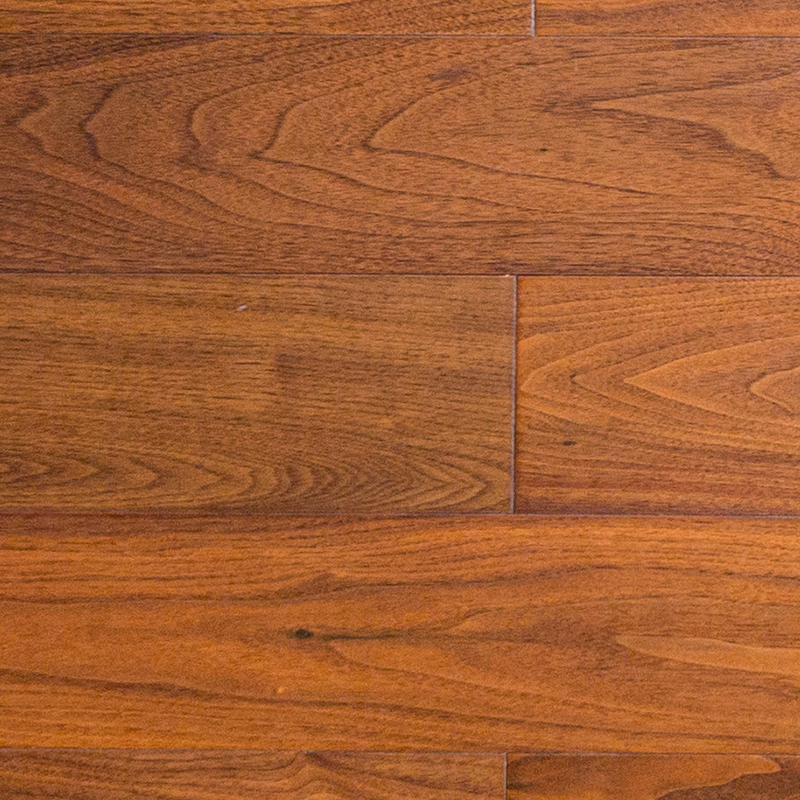
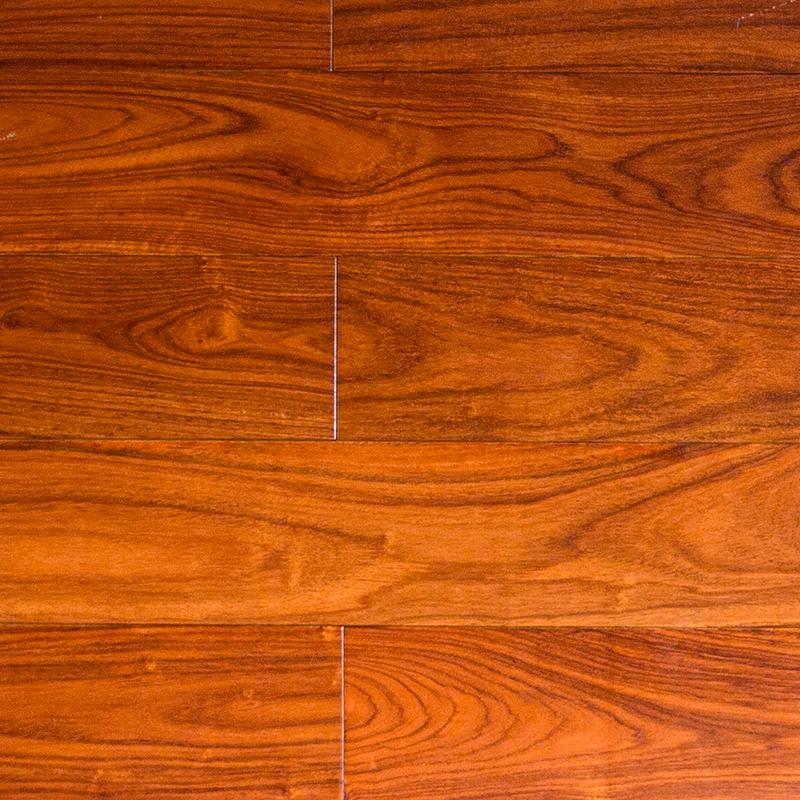
Wood species, moisture content, grade, and surface finish all influence how a chevron floor performs after installation. Suppliers should describe their species options, such as white oak, red oak, walnut, and teak, and explain how each is graded. Moisture content should be controlled within a defined range, which is especially important for projects that include underfloor heating. A floor cut accurately but dried inconsistently will shift after installation and open gaps at the point joints.
A complete chevron parquet production standards document should record these parameters in writing, including the acceptable range of natural variation in colour and grain.
A three-stage quality workflow
A reliable factory typically inspects product at three points. The diagram below summarizes a workflow that buyers can request in writing.
The sorting stage deserves particular attention. Chevron planks are not interchangeable between left-hand and right-hand orientation, and mis-sorting during production is one of the most common causes of failed installations. Ask whether the supplier labels or packs planks by hand orientation and how this is verified before cartons leave the factory.
Performance benchmarks to request
Dimensional tolerance on length, width, and thickness reported for each batch
Moisture content range for the finished product, supported by test records
Expected service life of at least 20 years under correct installation and maintenance
Confirmed compatibility with underfloor heating, including surface temperature limits
Waste Allowance and Budget Planning for Chevron Projects
Waste is the most frequently underestimated cost in chevron projects. Buyers who quote on net floor area without adding an allowance for mitred offcuts often discover a shortfall when the material reaches site. A conservative budget should be built from the room layout rather than from the area figure alone.
Bar heights reflect the upper end of each range, which is the safer reference for a first quotation. Practical budgeting steps include the following.
Measure the net area of each space, including recesses and angled walls that interrupt the pattern.
Count the pattern starting points, since each one consumes additional offcuts.
Apply the chevron range from the chart, selecting the upper end for rooms with many corners or irregular geometry.
Request a quotation that states the allowance explicitly so that the figure can be audited later.
Buyers who request a quote with a stated waste allowance and a clear reorder policy for matching batches avoid the two most expensive surprises in chevron procurement: material shortage and colour mismatch between delivery lots.
Custom Specification Options for Large Projects
Projects rarely fit standard catalogue specifications. A hotel may need a tone that matches its interior palette, a showroom may require a particular plank width for visual scale, and a residential development may demand a finish that tolerates heavy foot traffic. A capable manufacturer should be able to adapt the product within clearly defined limits.
Parameters that can be customized
Plank length and width adjusted to room proportions
Mitre angle at 45 degrees, 60 degrees, or a project-specific angle confirmed by sample
Wood grade selection from premium to rustic appearance
Surface finish including brushed texture, UV lacquer, UV oil, or wood wax oil
Edge treatment with beveled or non-beveled profiles
Colour range from light grey and pale yellow to dark brown and beige
OEM and ODM service with rapid prototyping of a sample board
Typical application scenarios
Custom chevron parquet is most often specified for private residences, boutique hotel lobbies, commercial showrooms, and luxury office interiors. In each case, the buyer benefits from requesting a pre-production sample and approving it under the project's actual lighting and finish conditions before full volume production begins.
Sample approval should be treated as a formal project milestone, with the approved sample retained as the reference standard for the entire order.
Certification and Export Documentation for Global Tenders
For projects that cross borders, documentation can determine whether a shipment clears customs and whether a tender submission is accepted. Buyers should request certificates early in the sourcing process rather than after the purchase order is confirmed. Documentation gaps are among the most common reasons for delayed delivery in international commercial projects.
FSC certification for sustainable and traceable wood sourcing
CE documentation for products placed on the European market
CARB Phase 2 emission compliance for formaldehyde content in wood-based materials
ISO quality management system certification covering production and inspection
Certificates should be current, issued for the specific product category, and traceable to the factory that will produce the order. Request copies rather than summaries, and confirm the validity period against the expected shipping window.
Project sourcing checklist
Confirm the waste allowance inside the quotation, using the chevron range as a reference point.
Define batch colour and grain consistency requirements for multi-container orders.
Agree on deliverables, including test reports, certificate copies, and installation guidance.
Specify the sample approval process and the acceptable range of natural wood variation.
Project Risk Controls: Where Chevron Orders Go Wrong
Most chevron problems originate upstream in the factory rather than on the installation site. Buyers reduce risk by asking suppliers to explain how each failure mode is prevented, not only how it is inspected after the fact.
Risk
Typical source
Control to request
Angle drift
Cutting station wear
Scheduled jig calibration with logged checks
Hand mix-up
Sorting error
Hand orientation labelled on every carton
Moisture swing
Uneven drying or storage
Recorded moisture readings for each batch
Colour mismatch
Mixed timber lots
Batch segregation and matched reorder policy
The point-to-point joint of a chevron floor has no overlap buffer. Minor dimensional or moisture-related movement will create a visible gap that cannot be concealed on site, which is why upstream control matters far more than correction during installation.
Ask any prospective supplier to describe its three most common production non-conformities and the corrective action taken for each. The answer reveals more about manufacturing maturity than any brochure.
Frequently Asked Questions
Q1: What is the main manufacturing difference between chevron and herringbone parquet for large projects?
Chevron planks are mitred at both ends and meet point to point, so the joint has no overlap to absorb small errors. Herringbone uses square-ended planks with a butt joint, which tolerates minor dimensional variation more easily. For large projects, chevron requires tighter angle control and more rigorous sorting throughout production.
Q2: What waste rate should I budget for chevron parquet flooring in my project quotation?
A common reference range is 15 to 25 percent, with the upper end appropriate for rooms with many corners, irregular walls, or multiple pattern starting points. The allowance should be stated explicitly in the quotation so that it can be reviewed and audited against the room layout.
Q3: What certifications are typically required for chevron parquet flooring exported to Europe and North America?
Buyers commonly request FSC certification for sourcing, CE documentation for European markets, CARB Phase 2 compliance for formaldehyde emissions in North America, and ISO certification for the quality management system. Copies should be current and traceable to the producing factory.
Q4: Which angle options are available for project-grade chevron parquet?
The most common options are 45-degree and 60-degree mitres. A 45-degree pattern gives a sharper, more pronounced V, while a 60-degree pattern visually elongates narrow spaces but generates a different waste profile. Project-specific angles are possible when confirmed through tooling and an approved sample.
Q5: Can chevron parquet flooring be customized in size, finish, and colour for hotel and commercial projects?
Yes, within defined manufacturing limits. Plank dimensions, mitre angle, wood grade, surface finish, edge profile, and colour range can usually be adapted. Buyers should approve a prototype under project lighting before committing to full production volume.
Q6: Why is batch consistency so critical when ordering large volumes of chevron parquet flooring?
Because the pattern runs continuously across the floor, colour and grain differences between delivery lots become visible at every joint. A matched reorder policy, batch segregation during production, and a written consistency tolerance are the most effective ways to protect a large installation from visible variation.


 English
 Español
 عربى

 Get Free Sample